
Introduction — a short shop story, some numbers, one question
I once stood beside a tired machine while a tech told me, “We treat each job like a new recipe.” I remember that because the tools felt alive—scraping, humming, precise. CNC turret lathe was the name we whispered when we wanted the work done fast and clean. In that same plant, throughput rose by roughly 22% after a single process change and scrap dropped nearly half (small wins, big smiles). So I asked: if simple shifts deliver that kind of lift, why do many shops still grind through the same bottlenecks day after day? This article slices into that puzzle, like filleting fish — careful, deliberate, and practical — and then points to what to try next.
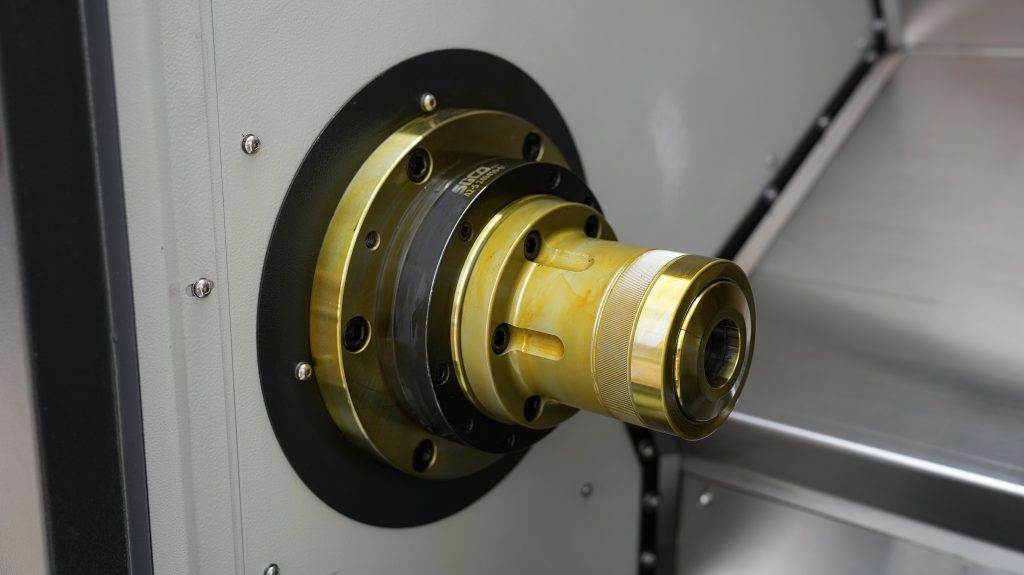
Deep Dive: Where traditional fixes fall short
I’ll be direct: many outfits patch problems with band-aid solutions. When teams say they need a vertical lathe for sale, they often mean they want brute force — a bigger spindle, more power. But replacing hardware without changing workflow keeps the root cause. On the shop floor, issues like repeated tool crashes or uneven surface finish usually trace back to control strategy, coolant system tuning, or slow tool changer cycles. These are not glamorous fixes. They are tuning, calibration, and, yes, some staff coaching.
Why does this still happen?
Part of it is familiarity bias. People buy a new machine and expect it to solve decades of process drift. It won’t. Servo motors and CNC controller mappings still need proper setup for the job. Live tooling must be matched to the feed rates. I’ve seen teams focus on cycle time numbers while neglecting setup and fixturing. Look, it’s simpler than you think — optimize the setup, not just the spindle. — funny how that works, right?
What’s Next: new principles for shops that want to lead
Moving forward means adopting a few core principles: modular tooling, closed-loop feedback, and predictable cycle modeling. I like to think of this as composing a menu: choose the right ingredients, test the seasoning, then scale the recipe. In practice, that looks like tighter integration between the CNC controller and live tooling, better tool libraries, and smarter coolant flow profiles. When a shop shifts this way, the same piece of equipment becomes more reliable and versatile.
Real-world impact?
Consider integrating a multi turret cnc lathe into a mixed-production line. You get parallel operations, reduced idle time, and fewer tool changes per cycle. I’ve seen a cell drop setup time by 40% when they rethought turret layout and tool grouping. That change also reduced chatter and extended tool life — more uptime, less waste. — honestly, small layout shifts compound into big savings.
Three practical metrics I use when advising shops
I’ll finish with three simple, measurable filters I recommend you use before buying or upgrading. First: Effective Cycle Yield — measure good parts per hour after setup stabilization. Second: Changeover Time to Qualified Part — time from job change to first good piece. Third: Tooling Utilization Rate — percentage of tool life used per shift (this tells you if your tool strategy is wasteful). If you track those, you’ll see cost and quality move together. I tend to weight the second metric a bit more in mixed-job environments; it often predicts throughput better than raw spindle speed.
We’re not chasing shiny specs. We’re tuning the whole system. If you want a partner with practical gear and hands-on setup help, take a look at Leichman. I’ve seen their setup teams help shops make those exact improvements — real results, not vaporware.